Do not change five parameters at once. Confirm material, nozzle condition/centering, optics cleanliness, standoff, focus, gas and speed in a controlled sequence so the actual cause can be identified.
Start with the cutting system, not only the parameter table
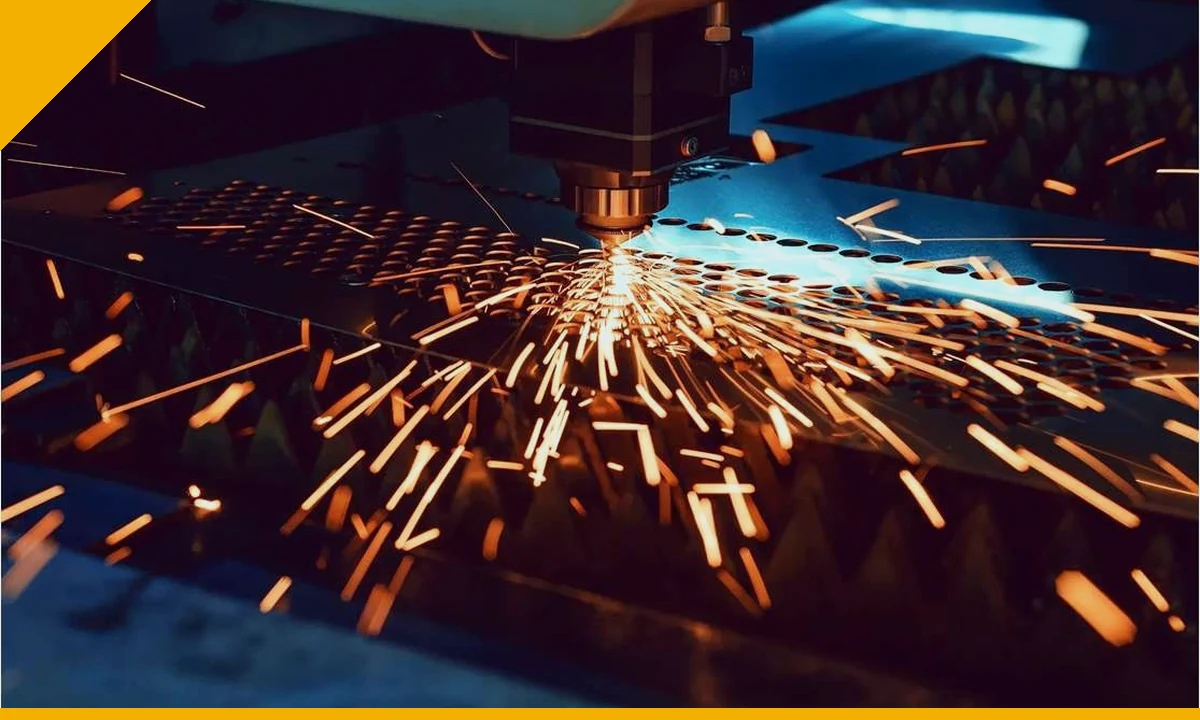
Laser cut quality depends on the interaction of beam, focus, nozzle, gas flow, material and motion. TRUMPF notes that focus position influences irradiance and kerf form, while nozzle diameter affects gas beam shape and quantity.
Heavy burr or dross
Possible contributors include incorrect focus, insufficient or unstable assist gas, damaged/contaminated nozzle, incorrect nozzle gap, speed mismatch, dirty optics or unsuitable parameters for the actual material condition. Confirm basics before increasing power.
Wide kerf
A wide kerf can be associated with focus position, beam condition, excessive heat input, incorrect optics/beam delivery or inappropriate speed. If the kerf changes by direction, investigate centering/alignment and nozzle condition.
Incomplete cut
- Verify material grade and actual thickness.
- Confirm assist gas pressure and supply stability.
- Inspect protective window/lens condition.
- Check nozzle for damage and concentricity.
- Confirm focus reference and standoff.
- Review speed and power against a known-good process window.
Piercing defects
Excessive spatter, crater size or failed piercing can damage the nozzle or protective optics. Check piercing mode, duration, focus, gas and nozzle condition, and inspect the upper surface after repeated pierce failures.
Consumables matter
The nozzle is part of the gas-delivery system, not just a copper tip. TRUMPF emphasizes precise nozzle geometry and concentricity because gas flow and distance regulation directly affect quality. The same principle applies across brands: use the correct nozzle type and verify centering after consumable work.
Recommended troubleshooting order
- Confirm material and thickness.
- Inspect nozzle and verify centering.
- Inspect protective optics.
- Check standoff/capacitive sensing.
- Verify gas type, pressure and flow.
- Verify focus reference.
- Run a controlled speed/power test.
- Record the result and keep the known-good combination.
This article is general guidance for preliminary engineering and shop-floor understanding. The drawing, applicable standard, machine/tooling OEM instructions, process-specific safety requirements and qualified engineering judgment take priority.