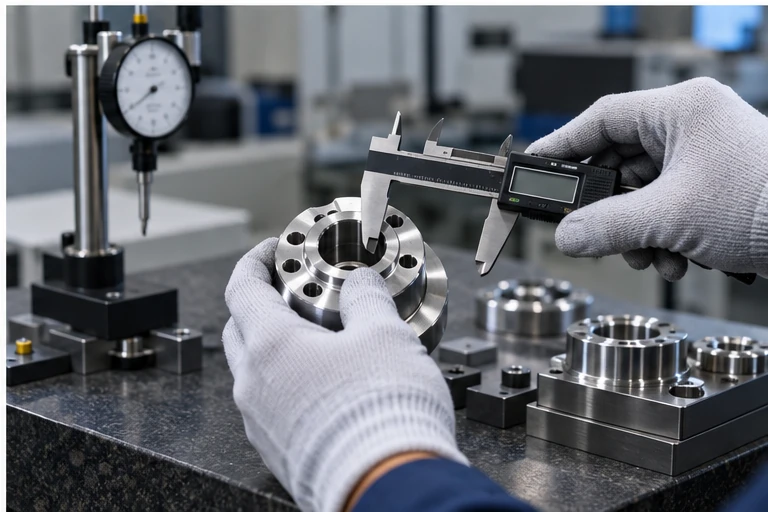
A caliper is only as good as the way it is held. Clean the jaws, check zero, align the jaws square to the feature, use light measuring force and repeat the reading until it is stable.
Start with the instrument, not the part
Before measuring, wipe the measuring faces and the workpiece. Close the jaws gently and confirm zero. On a conventional digital caliper, zeroing after closing the jaws is a good pre-check; an ABSOLUTE-type instrument retains its origin but should still be checked.
External measurement
Use the large outside jaws for thicknesses, outside diameters and widths. Keep the jaws square to the surfaces. When measuring a shaft, gently rock the caliper across the diameter: the correct reading is found when the jaws are aligned with the true diameter and the reading repeats.
Internal measurement
Use the smaller upper jaws. Insert them into the bore or slot, open them until they contact both sides, and align them with the true diameter. A tilted caliper can under-read an internal diameter.
Depth measurement
Use the depth rod with the beam seated flat on the reference surface. Keep the caliper body perpendicular to the hole or step. Chips, burrs and rounded edges can invalidate the result.
Reading a metric vernier
First read the last whole millimetre on the main scale before the vernier zero. Then find the vernier line that coincides with a main-scale line and multiply its index by the least count. A common metric vernier has a 0.02 mm resolution, but always read the actual instrument specification.
Common mistakes
- Measuring over burrs, dirt, oil film or damaged surfaces.
- Too much jaw pressure, especially on thin or soft parts.
- Tilting the jaws instead of keeping them square.
- Using a caliper where a micrometer or bore gauge is required by tolerance.
- Reading only once instead of checking repeatability.
When a caliper is not enough
A caliper is versatile, but it is not the right instrument for every tight tolerance. If the tolerance approaches the practical uncertainty of the caliper or if form errors matter, use a micrometer, bore gauge, height gauge, CMM or another appropriate measurement system.
This article is general guidance for preliminary engineering and shop-floor understanding. The drawing, applicable standard, machine/tooling OEM instructions, process-specific safety requirements and qualified engineering judgment take priority.